Build the furnace specification around the brazed assembly
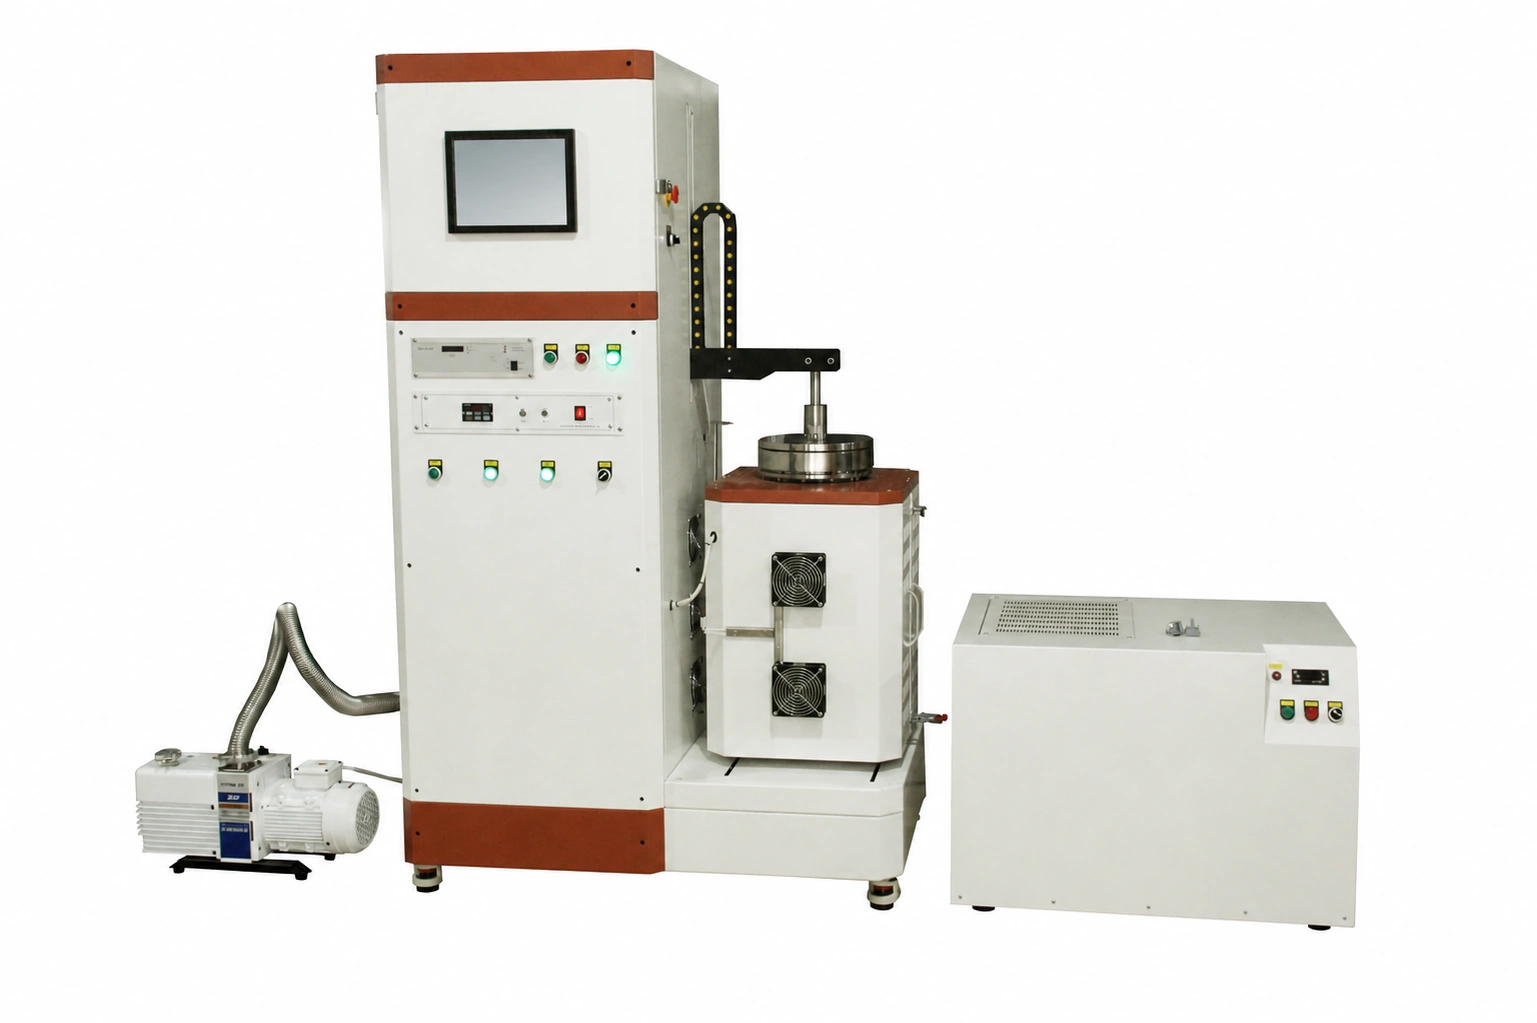
A vacuum brazing furnace is part of a complete joining process. Base materials, filler alloy, joint clearance, component cleanliness, fixture design, load orientation and the required thermal cycle all influence the equipment configuration. Pyrocore reviews these inputs before defining the hot zone, vacuum package, controls, loading arrangement and supply boundary.
Define the joint and filler-alloy process window
Provide the base-material grades, filler-alloy designation and intended joining route. Joint fit-up and cleanliness are process inputs, not furnace settings. If a current procedure exists, share the approved temperature-time sequence and acceptance method. For a new process, identify which parameters have already been established by trials and which still require development.
Size the usable hot zone from the complete fixture
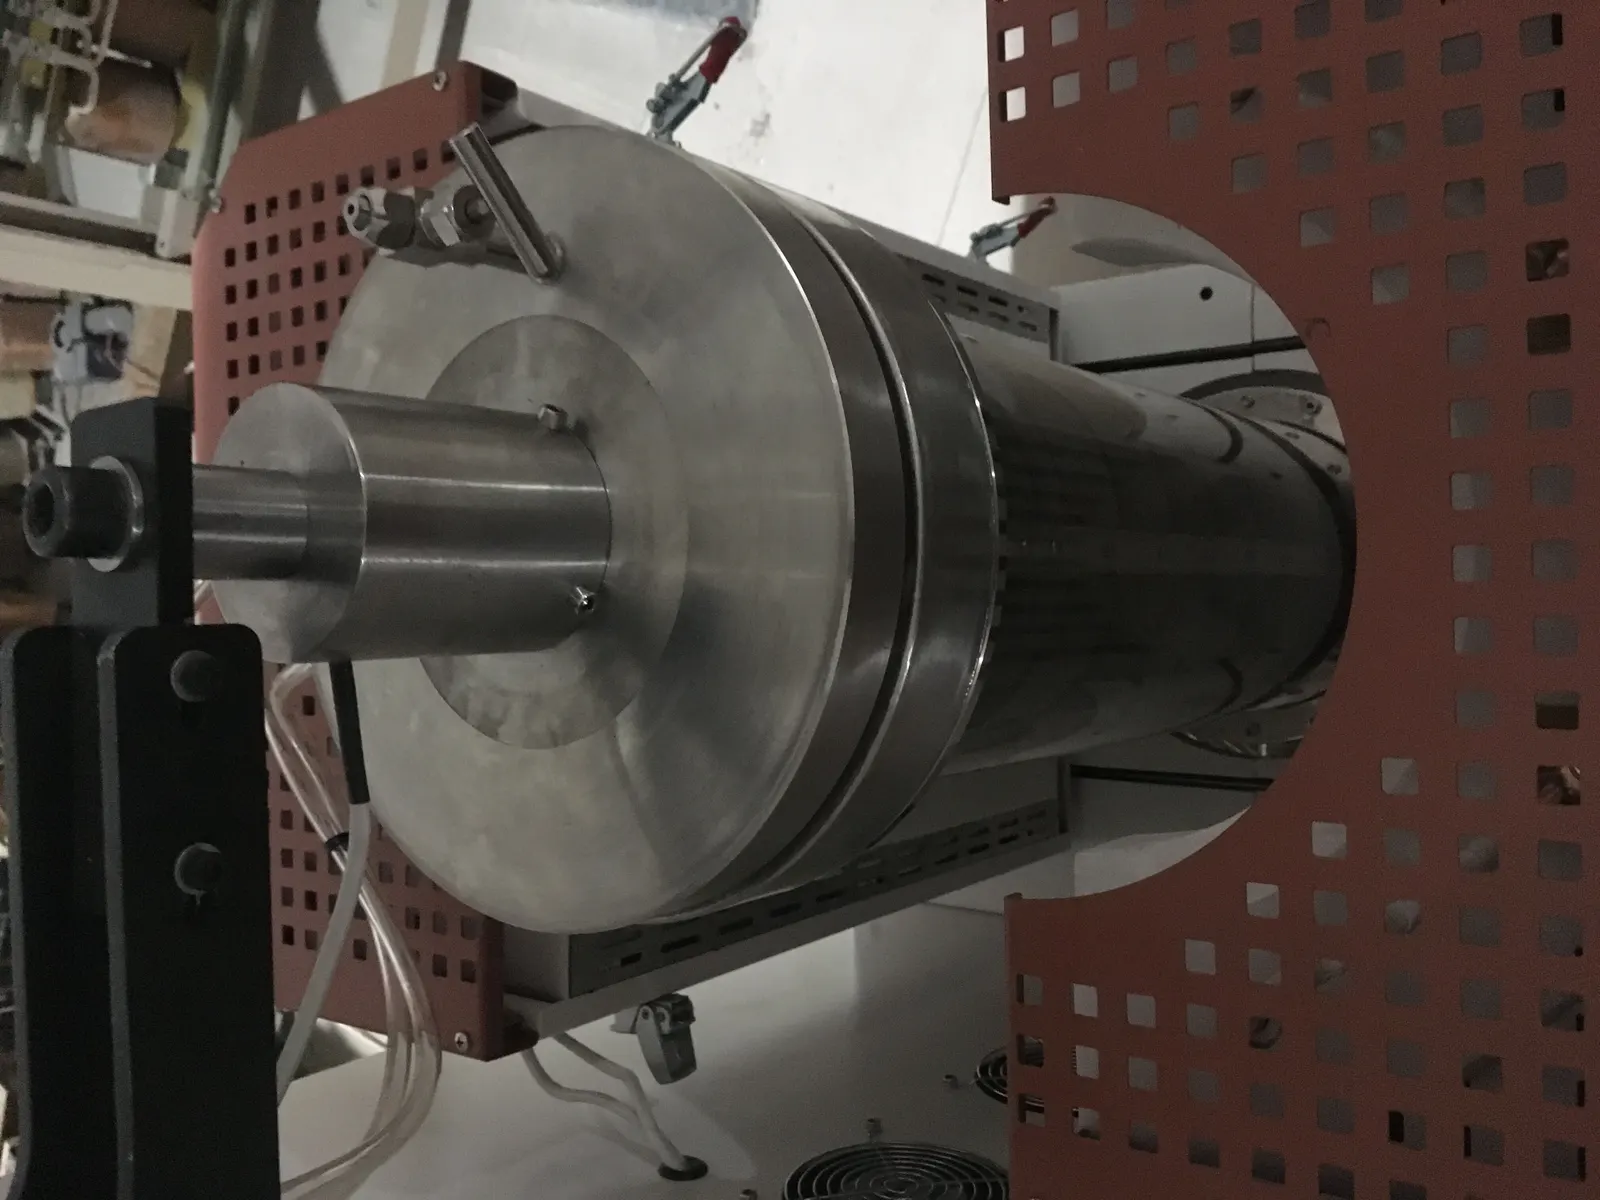
The largest workpiece dimension alone is not enough. Include fixture plates, baskets, supports, thermocouples and the clearances required for loading and uniform exposure. State the normal and maximum load mass, centre of gravity and loading direction. Pyrocore distinguishes the usable hot zone from the vessel, insulation and external machine dimensions.
Qualify pumping, backfill and cleanliness boundaries
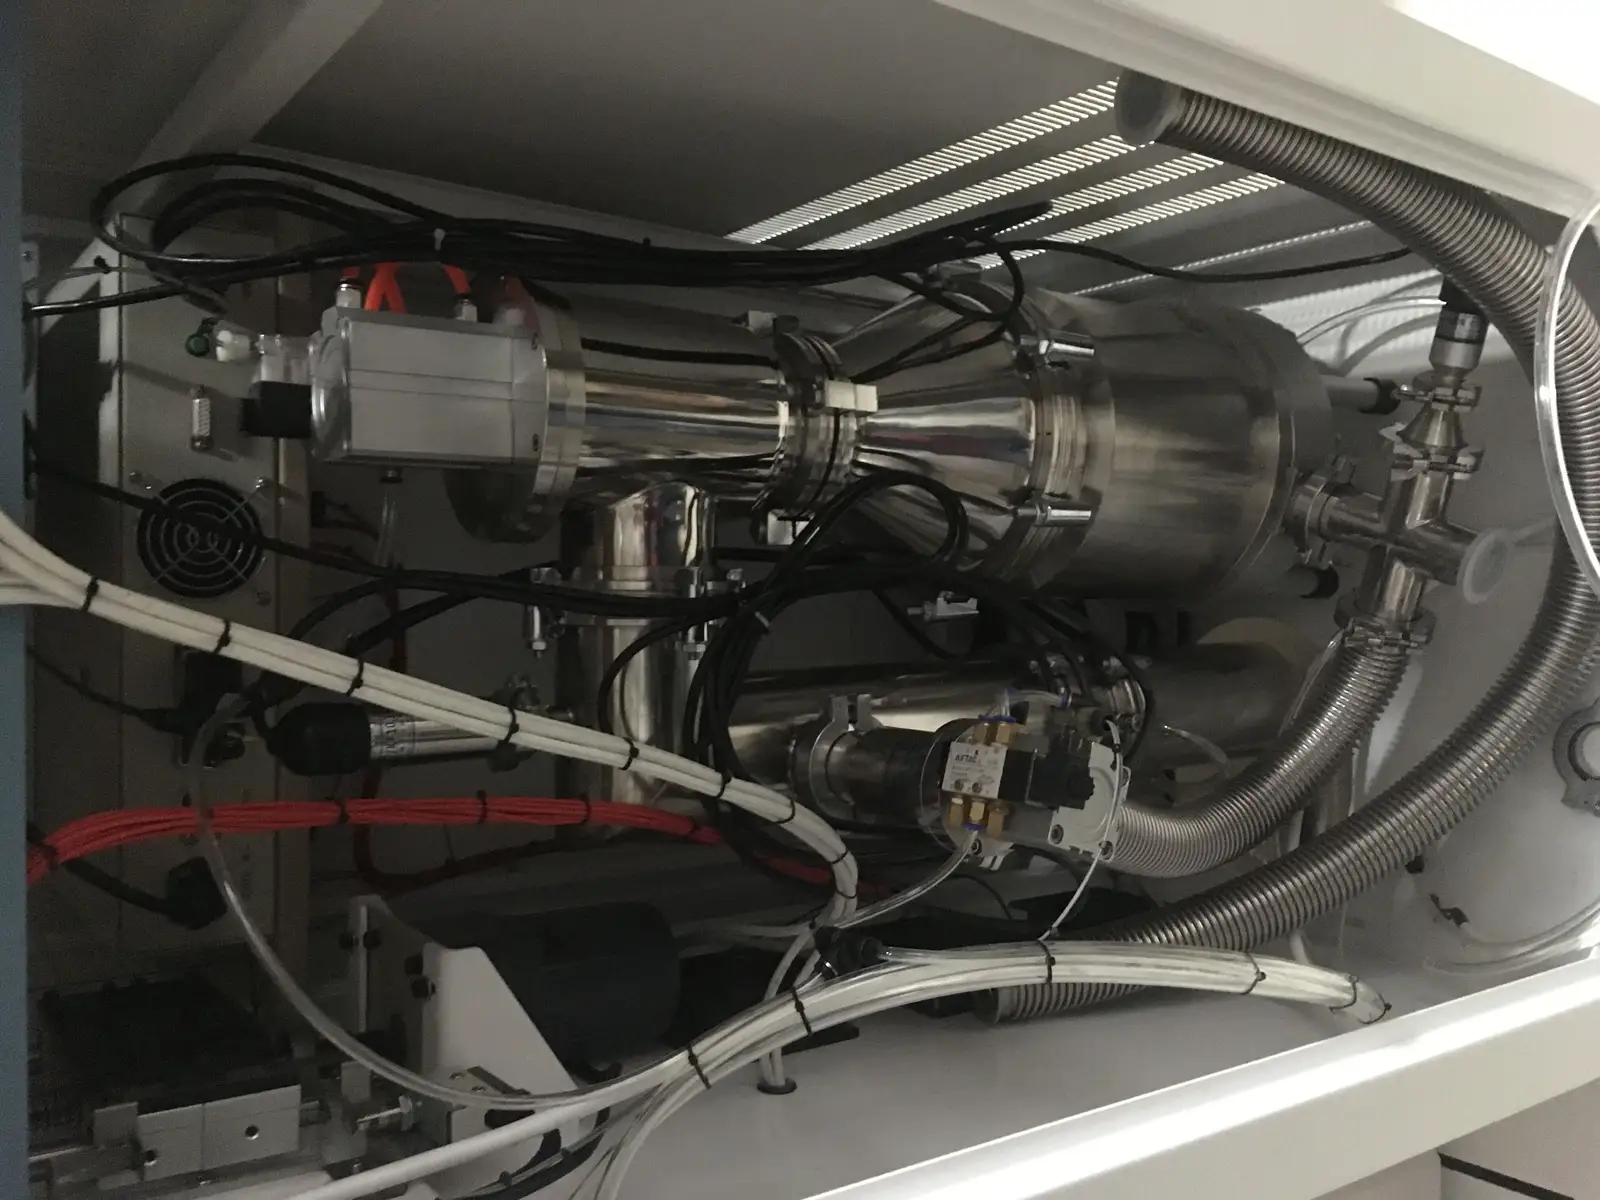
State the required process vacuum, expected outgassing, pumping sequence, permitted backfill gas and any pressure transitions used during the cycle. Oils, binders, surface treatments and trapped volumes can affect the vacuum duty. The pumping package, valves, gauges, vessel connections and exhaust route are therefore reviewed as one process system.
Coordinate heating, sensing and cooling
The heated zone and thermal shielding are selected around the load geometry and required cycle. Describe where process temperature must be represented, whether load thermocouples are used and which cycle records are required. Cooling expectations should be expressed as a process sequence and throughput requirement rather than a single furnace label.
Plan loading, controls and operating safeguards
Define how the fixture enters the vessel, the available handling equipment and the required operator clearance. The control sequence may coordinate heating, pumping, isolation, backfill and cooling stages. Required alarms, interlocks, recipe control, data logging and user access should be listed in the inquiry so they can be included in the project boundary.
Information required for a vacuum brazing furnace RFQ
- Base materials, filler alloy and joint description
- Assembly and fixture drawings with total load mass
- Normal and maximum production load
- Established or target thermal cycle
- Required process vacuum, backfill gas and cleanliness controls
- Loading method and available handling equipment
- Cooling and throughput expectations
- Power supply, utilities, destination and documentation requirements
For vacuum heat treatment without a brazing-specific process, compare the project boundary with Vacuum & Atmosphere Box Furnaces. For a custom heated interior, review Custom-Shaped Furnace Chambers.